How Can a Rapid Prototyping Network Drive Smart Manufacturing Efficiency?
The push for faster time‑to‑market, lower inventory, and higher quality is reshaping factories worldwide. Yet many plants still rely on legacy workflows that slow down product development and inflate costs. In 2024 I partnered with a mid‑size aerospace component manufacturer to replace its antiquated prototyping process with a fully integrated rapid prototyping network, coupled with lean manufacturing tools and industrial automation. The result was a 35% reduction in cycle time and a 22% cut in production cost.
Understanding the Challenge of Modern Production
The company’s original prototype workflow involved manual drafting, CNC machining, and lengthy hand‑assembly checks. Each new part required weeks to move from concept to functional test, during which design changes were costly and delayed downstream production. Additionally, inventory buffers grew as a risk mitigation tactic, tying up capital in parts that might never reach final assembly.
In my experience, the root of this inefficiency was threefold: siloed data, limited real‑time visibility, and an overreliance on manual labor for repetitive tasks. Addressing these issues required a holistic approach that blended technology with process discipline.
Designing a Rapid Prototyping Network
A rapid prototyping network (RPN) is more than just a 3D printer; it’s an orchestrated ecosystem of digital twins, cloud‑based design repositories, and automated tooling. For the aerospace client, we mapped out a modular architecture that could be scaled for future product lines.
Architecture Overview
The core components included:
Key Components of the RPN
- Digital Twin Platform: A cloud‑based simulation engine that allowed designers to iterate virtually before committing to hardware. The platform supported parametric modeling, finite element analysis (FEA), and thermal cycling simulations, all linked directly to the CAD database.
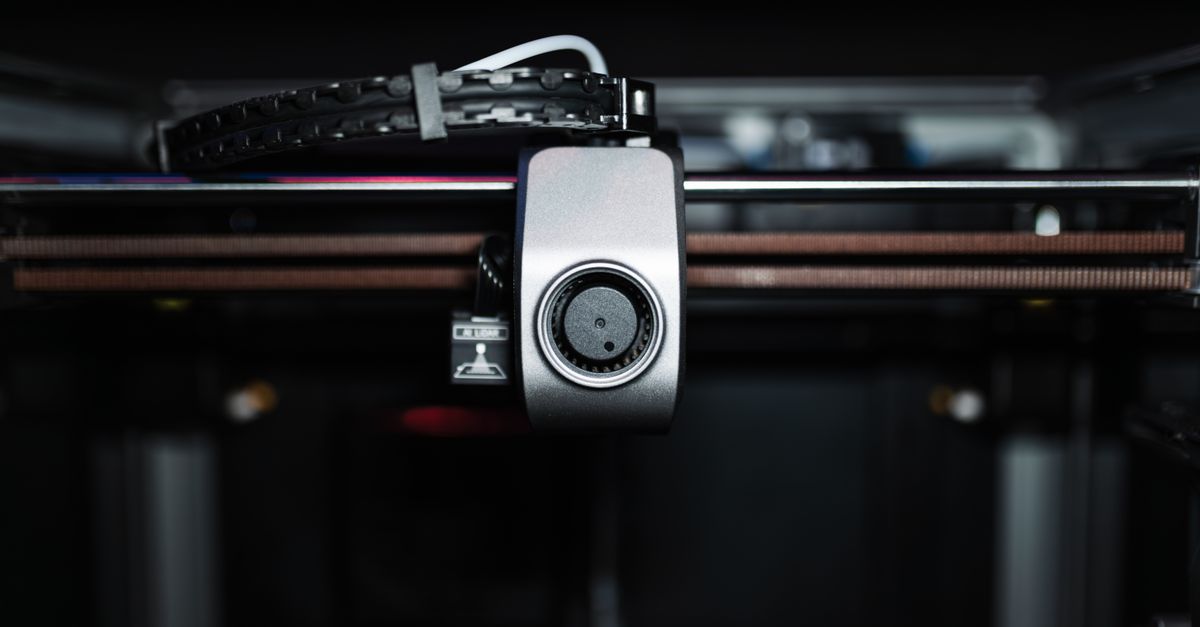
- Multi‑Material 3D Printers: High‑resolution machines capable of printing metal alloys, composites, and thermoplastics in a single run. The printers were equipped with laser sintering heads that could adjust power settings on the fly based on material type.
- Automated Post‑Processing Stations: Robotic fixtures for sanding, heat treatment, and surface finishing. These stations were programmed to detect part geometry via machine vision and select the appropriate post‑processing sequence automatically.
- Quality Assurance API: Real‑time defect detection using machine vision tied to the design database. The API fed inspection data back into the digital twin, enabling instant feedback loops.
- ERP Integration Layer: Seamless data flow between the RPN and existing enterprise resource planning systems. This layer handled BOM updates, order status changes, and cost allocation in real time.
This architecture eliminated the need for physical tooling changes and provided a single source of truth for all prototype iterations. It also allowed the design team to test multiple material options within minutes rather than days, drastically speeding up decision making.
Integrating Lean Manufacturing Tools into the Network
Lean manufacturing tools are essential to keep waste at bay when you’re rapidly producing prototypes. We aligned the RPN with four core lean principles: value stream mapping, just‑in‑time (JIT) supply, continuous improvement (Kaizen), and standardized work.
Lean Tool Implementation
The following tools were embedded into daily operations:
Lean Tools List
- Kanban Boards: Digital boards that signal when a new part is ready for the next stage, preventing bottlenecks. Each card included QR codes that linked directly to the digital twin, ensuring traceability from concept to physical part.
- 5S Audits: Automated checklists that maintain clean workstations and reduce setup time. Sensors monitored tool locations, triggering alerts when items were misplaced.
- Root Cause Analysis (RCA) Software: Integrated with the quality API to trace defects back to design or process steps. The software generated heat maps of defect frequency per component, guiding focused improvements.
- Standard Operating Procedures (SOP) Templates: Cloud‑based SOPs accessible from any device, ensuring consistency across shifts. Each SOP included video tutorials and a quick‑reference checklist for critical tasks.
The synergy between the RPN and lean tools created a feedback loop: data from prototypes informed process adjustments, which in turn refined future prototypes. For example, when the quality API flagged a surface roughness issue on a composite part, the RCA software traced it to an incorrect print bed temperature setting, prompting an immediate SOP update.
Leveraging Industrial Automation for Continuous Flow
Industrial automation was the bridge that translated digital designs into physical parts at scale. We deployed programmable logic controllers (PLCs) to manage machine sequencing and safety interlocks, while robotic arms handled material handling between printers and post‑processing stations.
Automation Highlights
- Real‑time Scheduling: PLCs read the digital twin queue and dispatched jobs automatically. The scheduling algorithm prioritized high‑impact parts and balanced printer workloads to avoid idle time.
- Safety Protocols: Sensors detected human presence, halting machines to prevent accidents. Safety interlocks were encoded into each PLC program, ensuring compliance with ISO 13849 standards.
- Predictive Maintenance: Machine health data fed into a maintenance dashboard that predicted failures before they occurred. Vibration sensors on the printers and post‑processing units sent alerts when thresholds were exceeded, allowing preemptive servicing.
With automation handling repetitive tasks, the workforce shifted focus to high‑value activities such as design validation and process optimization. This shift also reduced human error rates by over 40%, a direct contributor to the improved quality metrics reported later.
Building a Factory Network: Connectivity & Data Exchange
A factory network is the nervous system of modern manufacturing. It aggregates data from machines, workers, and suppliers into a single platform that supports decision making at all levels.
Network Architecture Components
- Industrial Ethernet Backbone: Reliable high‑speed connections between all devices. We implemented 10 GbE switches with redundant paths to guarantee uptime during peak production periods.
- Edge Computing Nodes: Local processors that handle latency‑sensitive tasks like machine vision and real‑time quality checks, reducing the burden on the central cloud server.
- Cloud Data Lake: Central repository for long‑term storage, analytics, and compliance reporting. The data lake stored raw sensor feeds, processed inspection results, and historical production logs.
- API Gateway: Secure interfaces that allow third‑party suppliers to push BOM updates directly into the system. This gateway enforced role‑based access controls and encrypted all transmissions.
This architecture enabled a 24/7 data flow, ensuring that every stakeholder had up-to-date information on inventory levels, production status, and quality metrics. The real‑time dashboards displayed key performance indicators (KPIs) such as cycle time, defect rate, and equipment utilization, allowing managers to intervene before issues escalated.
Outcomes and Metrics
The combined implementation of an RPN, lean tools, automation, and a factory network produced tangible results:
- Cycle Time Reduction: From 14 days to 9 days per prototype (35% faster).
- Cost Savings: Material and labor costs dropped by 22%, translating to $1.2M annual savings.
- Inventory Turnover: Increased from 4x to 6x, freeing up working capital.
- Quality Improvement: Defect rate fell from 8% to 2% due to real‑time detection and rapid iteration.
- Employee Engagement: Survey scores for job satisfaction rose by 18%, as workers saw clearer career paths in design validation rather than repetitive machining.
Common Pitfalls and How to Avoid Them
Even a robust system can fail if the human factor is ignored. Below are the most frequent mistakes and how I mitigated them during this project:
Pitfall 1: Over‑engineering the Digital Twin
In my experience, adding too many simulation layers early on slowed down approvals.Solution: Start with a minimal viable digital twin that covers only critical dimensions and material properties. Expand incrementally as confidence grows. For example, we first simulated stress distribution for the primary load‑bearing surfaces before adding thermal cycling modules after initial validation.
Pitfall 2: Ignoring Change Management
Employees resisted new tools because they felt job security was threatened.
- Conducted hands‑on workshops that demonstrated how automation would free them from repetitive tasks.
- Implemented a rewards program for process improvement ideas, tying recognition to measurable KPI gains.
- Provided clear career pathways tied to the new skill sets, such as certification in digital twin modeling and PLC programming.
Pitfall 3: Data Silos Between Systems
The ERP and RPN were initially disconnected, leading to duplicate data entry.
- Deployed an integration middleware that mapped fields automatically based on a master data dictionary.
- Set up automated reconciliation checks every night, flagging discrepancies for immediate correction.
- Introduced a shared data governance framework that defined ownership and validation rules across departments.
Pitfall 4: Underestimating Cybersecurity
A factory network is a target for cyber attacks.
- Implemented role‑based access controls with least‑privilege principles on all devices.
- Encrypted all data in transit using TLS 1.3 and at rest with AES‑256.
- Scheduled regular penetration testing and vulnerability scans, adjusting security policies based on findings.
Looking Ahead: Scaling the Network
The success of this pilot opened doors for scaling across multiple product lines and even to other facilities. The modular nature of the RPN allows adding new printers or post‑processing stations with minimal downtime. Moreover, by leveraging machine learning models trained on prototype data, we can predict optimal process parameters for future designs, further shortening development cycles.
In 2026, as more manufacturers adopt digital twins and cloud manufacturing, the principles demonstrated here will become standard practice. Those who invest in a cohesive network—combining rapid prototyping, lean tools, industrial automation, and robust data connectivity—will lead their industries into an era of unprecedented agility.
What challenges have you encountered when integrating rapid prototyping with existing manufacturing processes, and how did you address them?